Butt fusion fittings are essential components in various piping systems, particularly in applications where a reliable and leak – free joint is required. As a supplier of butt fusion fittings, ensuring the quality of our products is of utmost importance. In this blog, I’ll share some key methods and considerations for testing the quality of butt fusion fittings. Butt Fusion Fittings
Visual Inspection
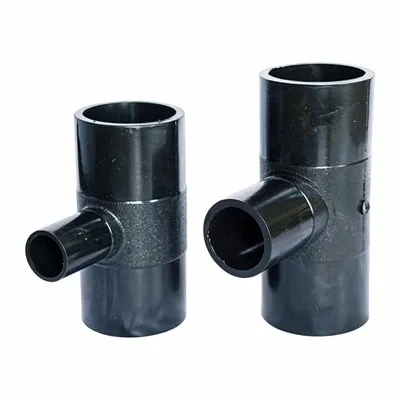
Visual inspection is the most basic yet crucial step in quality testing. When performing a visual check of butt fusion fittings, start by examining the surface finish. The fitting should have a smooth surface without any visible cracks, scratches, pits, or other defects. Cracks could lead to leaks in the future, while scratches might weaken the overall structural integrity of the fitting.
Inspect the dimensional accuracy of the fitting. This includes checking the outer diameter, inner diameter, and wall thickness. The dimensions should comply with the relevant industry standards. For example, in the case of polyethylene (PE) butt fusion fittings used in water supply systems, the dimensions need to meet the requirements set by standards such as ISO 4427 for PE pipes and fittings. Any deviation from the specified dimensions can cause issues during the butt – fusion process, resulting in improper joints.
Also, look at the color of the fitting. Consistent color throughout the fitting indicates a uniform manufacturing process. Unusual color variations might suggest a problem with the raw materials or the manufacturing process, which could potentially affect the quality of the fitting.
Mechanical Testing
- Tensile Testing: Tensile testing is a fundamental mechanical test used to evaluate the strength of butt fusion fittings. A sample of the fitting is subjected to a gradually increasing tensile force until it breaks. During this test, we measure the maximum stress the fitting can withstand before failure, known as the ultimate tensile strength. High – quality butt fusion fittings should have a sufficient ultimate tensile strength to withstand the pressure and forces exerted on them in the actual piping system. For instance, in a gas pipeline system, the butt fusion fittings must have a high enough tensile strength to prevent breakage due to internal gas pressure.
- Impact Testing: Impact testing assesses the ability of the butt fusion fitting to resist sudden impacts. There are different methods of impact testing, such as the Charpy impact test and the Izod impact test. In these tests, a pendulum is used to strike a notched sample of the fitting. The energy absorbed by the sample during the impact is measured. A high – quality fitting should be able to absorb a certain amount of impact energy without breaking. This is important because in real – world applications, the piping system might be subjected to impacts during construction, installation, or due to external factors like accidental blows.
- Flexural Testing: Flexural testing is used to determine the fitting’s ability to withstand bending forces. A sample of the fitting is placed on two supports, and a load is applied at the center. The test measures the maximum stress and deflection of the fitting under the bending load. This test is significant as butt fusion fittings in some piping systems may be subject to bending forces, for example, in underground piping where soil movements can cause the pipes and fittings to bend.
Thermal Testing
- Heat Deflection Temperature (HDT) Test: The HDT test is used to determine the temperature at which a butt fusion fitting begins to deform under a specific load. In this test, a sample of the fitting is heated at a controlled rate while a flexural stress is applied. The temperature at which the sample deflects a certain amount is recorded as the heat deflection temperature. This is important because in applications where the piping system is exposed to high temperatures, such as in some industrial processes or where hot water is being transported, the fitting needs to maintain its shape and integrity. A fitting with a low HDT may deform under high – temperature conditions, leading to leaks or a reduced service life of the piping system.
- Thermal Expansion Testing: Piping systems can experience temperature changes during operation. When the temperature rises, the materials expand, and when it falls, they contract. Thermal expansion testing measures the amount of expansion and contraction of the butt fusion fitting over a specific temperature range. This information is crucial for proper installation of the piping system. If the thermal expansion of the fitting is not properly accounted for, it can cause stresses in the joints, leading to joint failure over time.
Chemical Analysis
The chemical composition of butt fusion fittings is a key factor in determining their quality. Chemical analysis can be performed using various techniques such as spectroscopy or chromatography. For example, in the case of PE butt fusion fittings, the analysis can determine the density, molecular weight distribution, and the presence of any additives.
The density of PE affects its mechanical properties. Higher – density PE generally has better stiffness and strength, while lower – density PE has better flexibility. The molecular weight distribution also plays a role in the performance of the fitting. A narrow molecular weight distribution usually indicates a more uniform material with better mechanical and processing properties.
Additives in the fitting can serve different purposes. For example, antioxidants are added to prevent the oxidation of the material, which can extend the service life of the fitting. UV stabilizers are used when the fitting is exposed to sunlight to prevent degradation due to ultraviolet radiation. Chemical analysis can ensure that the right amount and type of additives are present in the fitting.
Fusion Welding Quality Testing
Since butt fusion fittings are joined using the butt – fusion welding process, the quality of the weld is a critical factor.
- Visual Inspection of Welds: After the fusion welding process, a visual inspection of the welds is the first step. The weld bead should be uniform in appearance and have no visible defects such as porosity, cracks, or incomplete fusion. The bead should have a smooth transition from the base material to the weld area.
- Destructive Testing of Welds: Destructive testing methods can be used to further evaluate the quality of the weld. For example, a section of the welded joint can be cut and examined under a microscope to check for internal defects, such as lack of fusion between the two mating surfaces. Another method is to perform a peel test on the welded joint. In this test, the two parts of the welded fitting are pulled apart to assess the strength of the weld.
Quality Testing Standards and Certification
In addition to the above – mentioned testing methods, it is important to adhere to relevant industry standards and obtain appropriate certifications. For example, in Europe, products may need to comply with standards such as EN 12201 for plastic piping systems. In the United States, standards like ASTM D3350 for PE raw materials are widely followed.
Certifications such as ISO 9001:2015, which is a quality management system standard, can provide assurance to customers that the manufacturing process of the butt fusion fittings is well – controlled and follows strict quality procedures. Other specialized certifications, such as WRAS (Water Regulations Advisory Scheme) certification for fittings used in potable water systems, indicate that the product meets the specific requirements for water – contact applications.
As a supplier of butt fusion fittings, we are committed to providing high – quality products. Our strict quality control process, which includes all the above – mentioned testing methods, ensures that our fittings meet and exceed industry standards. We understand that the quality of our products directly impacts the performance and safety of the entire piping system.
Electrofusion Fittings If you are in need of high – quality butt fusion fittings, you can reach out to us to discuss your procurement needs. Our team of experts is ready to provide you with detailed information about our products, testing procedures, and to assist you in finding the most suitable fitting for your application. Let’s work together to ensure the success of your piping projects!
References
- ISO 4427: Plastics pipes and fittings for water supply – Polyethylene (PE) – Specifications
- ASTM D3350: Standard Specification for Polyethylene Plastics Pipe and Fittings Materials
- EN 12201: Plastics piping systems for water supply – Polyethylene (PE) – General requirements
- ISO 9001:2015 – Quality management systems – Requirements
Qingdao Polyfusion Machinery Co., Ltd.
As one of the most professional butt fusion fittings manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please feel free to buy bulk high quality butt fusion fittings from our factory.
Address: Chengyang Industry Zone, Chengyang, Qingdao, Shandong, China
E-mail: export01@qdpolyfusion.com
WebSite: https://www.polyfusionfittings.com/
